High Quality Pipe Machine Equipment is more than polished steel, a powerful motor, or an attractive product brochure. It is a complete production system that delivers stable results under real factory conditions. A reliable machine should form pipes accurately, maintain consistent wall thickness, and reduce unnecessary material waste. Operators should also find its controls clear, responsive, and safe during long production shifts.
Look closely at the details. Rollers must align correctly. Welding units need steady energy output. Cutting systems should produce clean, repeatable ends. Sensors, bearings, and hydraulic components must withstand heat, dust, vibration, and continuous use. A bright machine frame proves little. Performance records, maintenance access, testing procedures, and after-sales support reveal much more.
Quality expert W. Edwards Deming stated, “Quality comes from the improvement of the production system, not from inspection.” This principle remains highly relevant to pipe manufacturing. High Quality Pipe Machine Equipment should prevent defects through accurate design, careful calibration, operator training, and continuous monitoring. It should not merely identify poor pipes after production.
Experienced buyers may examine sample pipes, review tolerance data, and observe a complete production cycle before purchasing. They should ask difficult questions about spare parts, software updates, energy consumption, and service response times. Some manufacturers may promise perfection. That claim deserves reflection. Even excellent equipment requires skilled operators, planned maintenance, and suitable raw materials. The following outline examines these practical indicators and explains how businesses can distinguish dependable pipe machinery from equipment that only appears impressive.
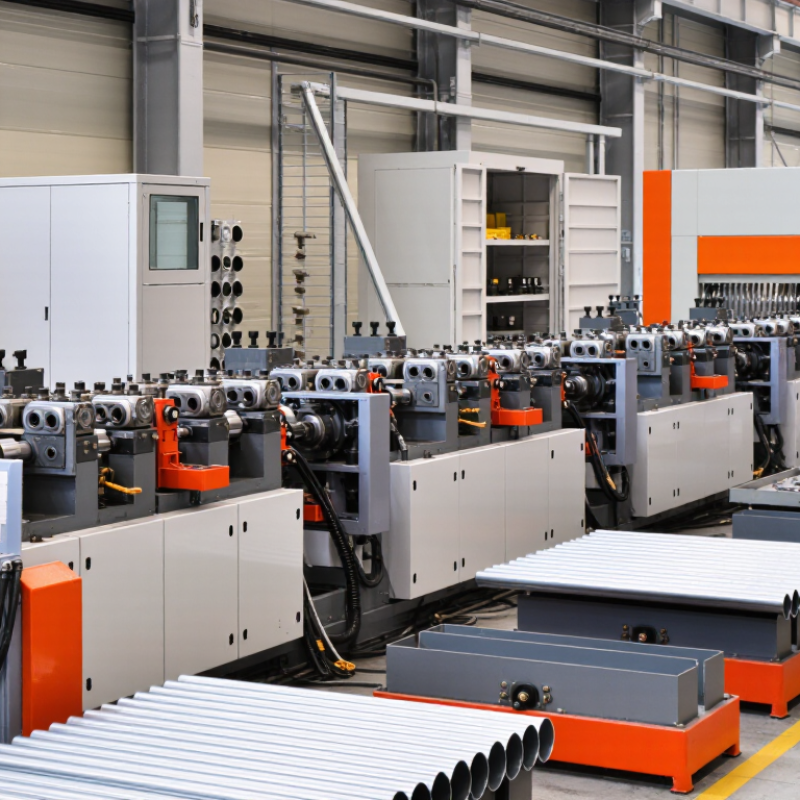
High-quality pipe machine equipment is defined by repeatable performance, not polished brochures. In modern manufacturing, dimensional accuracy, stable feeding, and consistent forming quality matter every production day. A reliable machine should hold tight tolerances across different pipe materials and wall thicknesses. Its control system must record speed, temperature, pressure, and fault conditions clearly. Operators need fast adjustments, guarded moving parts, and accessible maintenance points.
Deloitte’s 2024 Smart Manufacturing and Operations Survey reported that 86% of manufacturers view smart manufacturing as important for competitiveness. This supports connected equipment with traceable production data, remote diagnostics, and practical energy monitoring. McKinsey research estimates predictive maintenance can reduce downtime by 30% to 50%. However, sensors alone do not create quality. Poor calibration can produce impressive dashboards and defective pipes. That weakness is easy to overlook.
A strong evaluation also examines lifecycle performance. Check spare-part availability, software support, calibration procedures, and technician training before purchasing. The U.S. Department of Energy reports that compressed-air leaks can waste 20% to 30% of compressor output, making pneumatic efficiency worth measuring. Noise, vibration, scrap rates, and changeover time should be tested during real production conditions. No machine is perfect. The best equipment makes its limits visible, supports corrective action, and improves steadily through documented feedback.
| Evaluation Dimension | Practical Quality Benchmark | Typical Data or Range | How to Verify | Manufacturing Benefit |
|---|---|---|---|---|
| Dimensional accuracy | The machine maintains stable outside diameter, wall thickness, length, and ovality during continuous production. | Example target for precision tube production: diameter tolerance of approximately ±0.10% to ±0.25%; wall-thickness tolerance commonly around ±7.5% to ±10%, depending on product standard and process. | Measure samples with calibrated micrometers, laser gauges, or coordinate measuring equipment at start-up and at defined production intervals. | Reduces rejected material, improves downstream fit, and supports consistent product certification. |
| Line speed and throughput | The line reaches its rated speed without excessive vibration, overheating, surface damage, or dimensional drift. | Representative operating speeds vary widely: roughly 10–30 m/min for heavy-wall or large-diameter pipe and 30–120 m/min for smaller, thinner-wall tube, depending on material and forming method. | Run a documented acceptance test using the intended material, dimensions, tooling, and production recipe. | Increases productive capacity while keeping output predictable. |
| Weld or joint integrity | The forming and joining system produces a uniform seam or joint with controlled heat input and repeatable alignment. | Verification may include 100% visual inspection, eddy-current or ultrasonic testing, and destructive tests such as flattening, bend, or tensile testing when required by the applicable product standard. | Review weld-bead appearance, non-destructive test results, and mechanical-test records from a full production trial. | Improves pressure resistance, service life, and customer confidence. |
| Process control | Sensors and control software maintain forming force, temperature, speed, tension, and welding parameters within defined limits. | Critical parameters should be monitored continuously, with alarm limits, recipe management, trend displays, and recorded production data. | Check calibration records, data logs, alarm history, password permissions, and repeatability across several batches. | Makes quality less dependent on operator experience and supports traceability. |
| Mechanical rigidity | The frame, shafts, rolls, guides, and bearings resist deflection and maintain alignment under rated load. | A quality evaluation should confirm stable alignment under operating load, low vibration, and no abnormal shaft or bearing temperature rise. | Inspect foundation drawings, alignment reports, vibration readings, bearing temperatures, and load-test results. | Protects tooling, reduces surface defects, and extends machine service life. |
| Tooling flexibility | The equipment accommodates the required diameter, wall-thickness, material, and profile range with controlled changeover. | A practical design may support multiple product sizes through interchangeable rolls, guides, dies, or forming cassettes; actual range depends on machine architecture. | Confirm the approved size matrix, tooling drawings, changeover procedure, and first-off dimensional results. | Improves product variety and reduces the need for separate production lines. |
| Changeover efficiency | Tooling adjustments are accessible, repeatable, and supported by documented setup values. | Well-designed lines commonly target approximately 30–120 minutes for a planned size change, although heavy tooling and large product ranges may require longer. | Time at least three complete changeovers and record setup time, scrap during start-up, and first-pass acceptance. | Reduces downtime, setup waste, and production scheduling constraints. |
| Energy efficiency | Motors, drives, heaters, cooling systems, and compressed-air circuits are correctly sized and monitored. | Track electricity consumption in kWh per tonne or kWh per 1,000 metres; the actual value changes significantly with material, diameter, wall thickness, speed, and joining process. | Use production-grade power meters during a stabilized trial and compare energy use at different operating rates. | Lowers operating cost and helps establish measurable environmental performance. |
| Reliability and availability | The machine operates consistently between planned maintenance events and provides accessible service points. | Use availability as a site-specific KPI: Availability = planned production time minus unplanned downtime, divided by planned production time. | Review maintenance history, mean time between failures, mean time to repair, spare-parts lead times, and downtime codes. | Improves delivery reliability and total cost of ownership. |
| Safety engineering | Moving parts, hot surfaces, electrical systems, and stored energy are protected through guarding, interlocks, emergency stops, and documented risk assessment. | Safety design should follow a documented risk-reduction process consistent with recognized machinery-safety practices, including ISO 12100 principles where applicable. | Perform a safety acceptance audit covering guards, interlocks, emergency-stop response, lockout procedures, signage, and operator training. | Reduces injury risk, regulatory exposure, and unsafe machine interventions. |
| Quality assurance and traceability | Raw-material identity, process conditions, inspection results, and finished-product status can be linked to a production batch. | A robust system records coil or billet identification, operator, recipe, timestamp, test results, nonconformities, and release status. | Audit electronic or paper records and trace one finished batch back to its raw material and process history. | Supports root-cause analysis, customer audits, and controlled corrective action. |
| Maintenance and supportability | Wear parts are identifiable, lubrication points are accessible, and service instructions are clear and current. | Required documentation should include manuals, electrical diagrams, pneumatic or hydraulic schematics, recommended spares, lubrication intervals, and troubleshooting procedures. | Check document completeness, spare-parts interchangeability, training records, and response procedures for common failures. | Shortens repair time and preserves long-term machine performance. |
| Acceptance testing | Performance is proven under agreed production conditions rather than evaluated only from design specifications. | A complete test should cover output rate, dimensional capability, surface quality, seam or joint integrity, changeover, safety functions, and data capture. | Use a signed factory or site acceptance protocol with defined samples, tolerances, test duration, and pass/fail criteria. | Creates objective evidence that the equipment meets the manufacturing requirement. |


© Copyright 2025 | LittleFirefighter.com | All Rights Reserved | 1EZ Creative: Orange County Web Design